0
  •  x 
No products in cart

BLOG

Q) The plasma power  is not starting when the CNC is in plasma mode, But if you set the CNC in flame mode the Plasma power source ignites.
 
A) The problem is caused because the CNC parameter is not set correct. Make sure in PLASMA parameters set the ARC ON M ORDER as 12 and ARC OFF M ORDER as 13. This should be set like this always never change.

Q:- How to connect my plasma power generator  to the CNC small cutting machine.
A:- There are six wires to connect between plasma and CNC.
         START:-2 wires
         FINISH:- 2 wires
         ARC+:- 1 wire
         ARC-:- 1 wire
Refer your plasma power generator manual for details for connection

Signal Type Note
CNC START output Normal open: dry contact closure; used for torch ignition.
CNC START
DIV ARC+ Input Receive the signal of raw arc voltage from plasma. Can receive the arc voltage from 50VDC to 300VDC.
DIV ARC-
DIV FINISH Input Normal open: dry contact closure; Receive the signal of OK TO MOVE from plasma; it is the signal sent by plasma source to CNC machine, to give the feedback that the torch is well ignited and ready to move.
DIV FINISH


 Our service team will help you connect any plasma model to the SteelTailor CNC
You can contact the service team via email:-   This email address is being protected from spambots. You need JavaScript enabled to view it.
Also contact us via Skype: service-steeltailor

Q, Can we use PMX plasma machine 125 with SteelTailor machines, with ST-THCEX 03 height control.

A, The old THC model the ARC voltage range is not be suitable with PMX 125 AARC voltage range.  The torch diameter of PMX 125 is bigger compared to other PMX series machine so need to change the torch holder. You can use our new THC “ST-THC EX 03A” which is compatible for PMX 125.


Q:What is CNC cutting machine steel plate correction?

A:When the CNC cutting machine is used for cutting the steel plate, especially the thick or large steel plate, it is difficult that the steel plate and CNC cutting machine keep parallel, resulting in the cutting failure or serious steel waste. The correction of steel plate means that the controller automatically rotates the input cutting graph after obtaining the angle of steel plate to adapt to the offset angle of steel plate. 


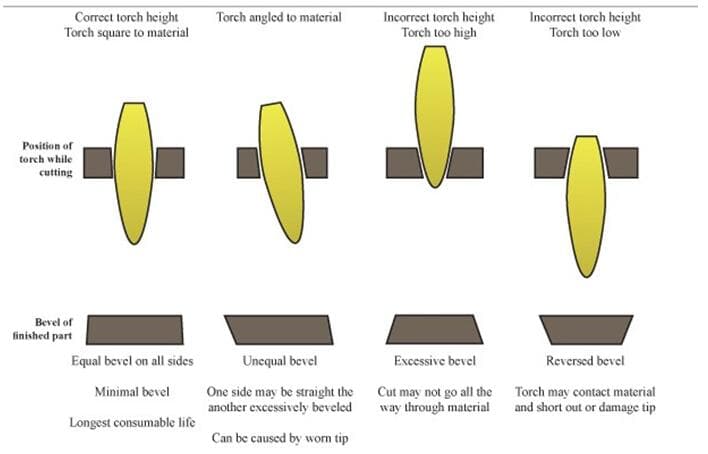
Q) When we are using plasma cutting the edge of the cutting is not good, may ways to improve the quality?
 
A)
 The plasma cutting quality depend up on many things, the torch parts, air quality, cutting speed, plasma current. The main external factor is the air quality.  If the air you supply for plasma has oil or water in it will cause the cutting quality and cause reduction in torch consumables life, It is better to have a dust, oil, water filter to be fix in the gas inlet for plasma so that the air quality improves.

Q) Do you have a cutting parameter table for flame cutting operation?
 
A) Yes, you can refer the installation manual last section for details   for cutting parameter for flame cutting. If you need more details please contact our technical support team. The preheat time and the pierce time is not given in the table because it depend up on you local environment and the cutting gas quality. This setting the operator should judge and set by himself. 

Customer Center

Call. +86-10-51662600
Email. info@steeltailor.com

Cannes Industrial Park, No.18 Shuang Qiao Dong Lu, Chao Yang District

Beijing ,China. 100121